Site Search
Search products, specifications, technical resources and documentation
Stainless Steel Material Verification & Alloy Integrity
Eliminate alloy mix-ups, premature corrosion, and mesh failure. Every batch of woven wire mesh manufactured and supplied by MutualFilter undergoes strict metallurgical verification, heat-number traceability, and optical dimensional screening.
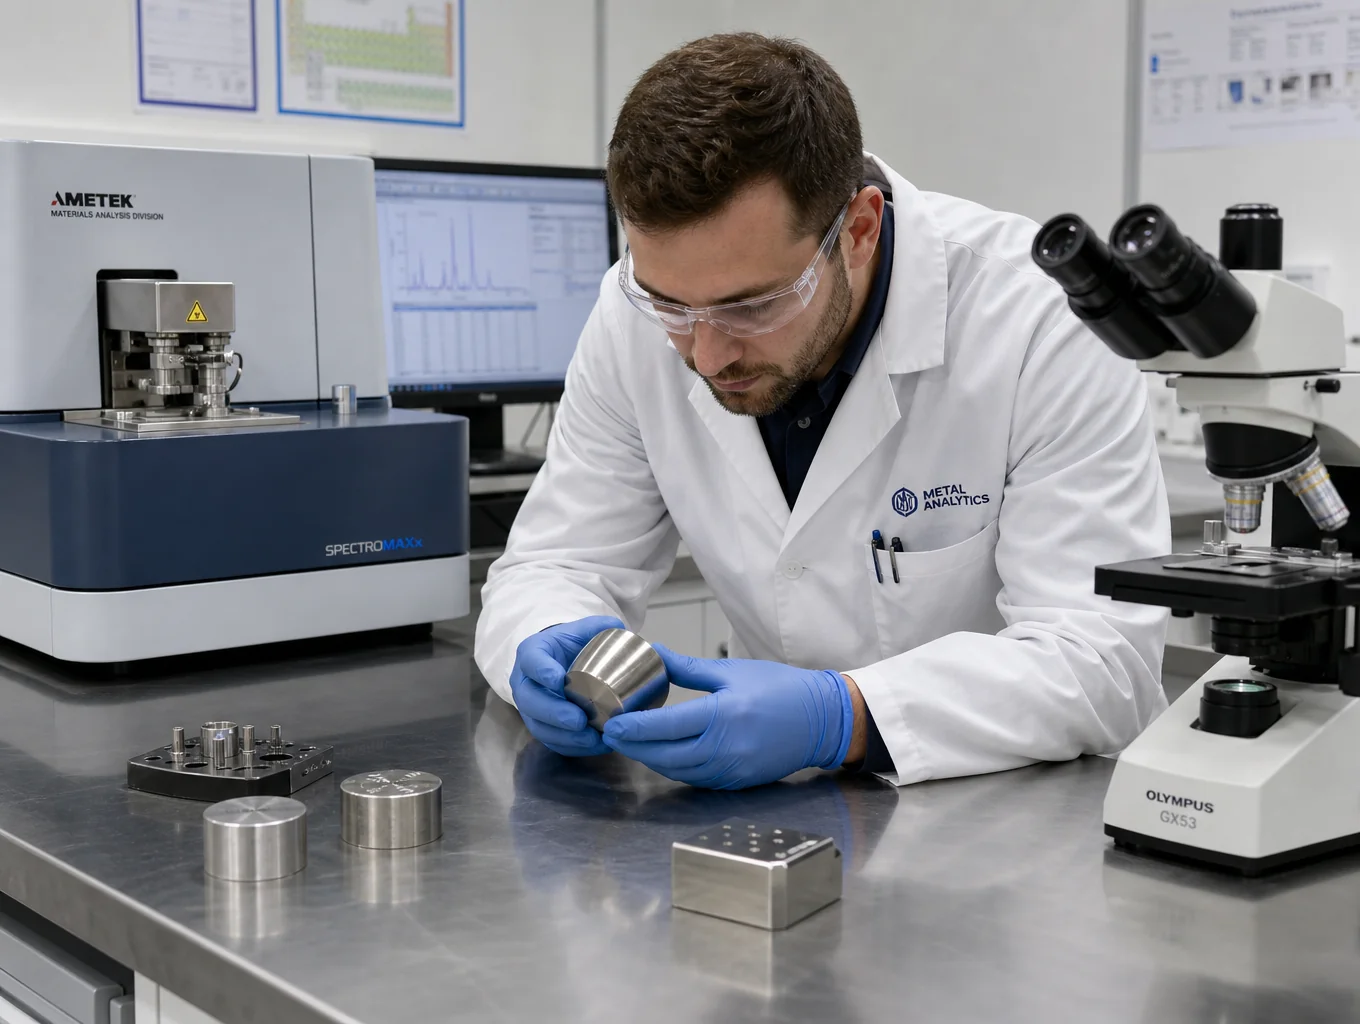
Standard Alloy Composition Limits
Spectrometry| Alloy Grade | Chromium (Cr) | Nickel (Ni) | Moly (Mo) |
|---|---|---|---|
| AISI 304 / 304L | 18.0 - 20.0% | 8.0 - 12.0% | - |
| AISI 316 / 316L | 16.0 - 18.0% | 10.0 - 14.0% | 2.0 - 3.0% |
| AISI 904L | 19.0 - 23.0% | 23.0 - 28.0% | 4.0 - 5.0% |
| Alloy 20 / Inconel | 19.0 - 21.0% | 32.0 - 38.0% | 2.0 - 3.0% |
Three-Tier Verification Architecture
Standard operational procedures applied across all wire mesh weave specifications.
Positive Material Identification (PMI)
100% handheld XRF elemental spectroscopy verifying Cr, Ni, Mo alloy composition before and after weaving.
EN 10204 3.1 Inspection Certificates
Complete heat traceability back to master coil melt source with mechanical and chemical test reports.
Optical Aperture & Wire Diameter Scan
Automated calibrated camera systems measuring mesh count, wire uniformity, and aperture geometry.
Stainless Steel Material Verification Process
MutualFilter enforces a strict multi-tier verification regimen across all wire alloys. From melt heat authentication to non-destructive alloy spectroscopy and automated aperture scanning, every specification is proven before shipment.
Four-Tier Verification Workflow
Sequential quality checkpoints applied to standard rolls, slit coils, and engineered components.
- Mill Test Certificate (EN 10204 Type 3.1) cross-referencing
- Heat lot traceability logging and positive stock quarantine
- Master coil optical surface defect and gauge pre-screening
- Handheld XRF and Optical Emission Spectrometry (OES)
- Strict Ni, Cr, Mo, and C tolerance validation (304L, 316L, 904L)
- PREN (Pitting Resistance Equivalent Number) certification
- Tensile strength (Rm) and yield strength (Rp0.2) pull tests
- Elongation rate (A50mm) and wire ductility assessment
- Surface hardness testing per ASTM E18 standards
- Digital image analysis for mesh count, aperture size, and wire diameter
- Ultrasonic degreasing and surface free-iron passivity testing (ASTM A967)
- Batch-specific EN 10204 3.1 MTR inspection dossier issuance
| Inspection Domain | Testing Methodology | Governing Standard | Measured Parameters |
|---|---|---|---|
| Chemical Verification | XRF & Optical Emission Spectrometry | ASTM E1086 / ASTM E1476 | Full elemental composition (Cr, Ni, Mo, C, S, P) |
| Mechanical Tensile | Universal Tensile Pull Tester | ISO 6892-1 / ASTM A580 | Tensile Strength, Yield Proof, Elongation % |
| Dimensional Mesh Geometry | High-Resolution Optical Vision System | ISO 9044 / ASTM E2016 | Mesh Count, Warp/Weft Aperture, Wire Caliper |
| Surface Passivation | Ferroxyl & Copper Sulfate Testing | ASTM A967 / ASTM A380 | Free iron contamination & passive film integrity |
| Pore Size Distribution | Capillary Flow Porometry (Bubble Point) | ASTM F316 / ISO 4003 | Absolute micron rating, bubble point pressure |
100% Raw Heat Traceability
Every roll and fabricated filter screen is mapped to original melt heat numbers, preventing mix-ups.
Non-Destructive PMI Testing
Field and benchtop X-ray fluorescence (XRF PMI) alloy verification is available for applicable products and specific orders upon request.
EN 10204 3.1 Certification
Complete formal inspection documents including independent chemical and mechanical test records.
ISO 9044 Class Compliance
Rigorous aperture tolerance controls matching European and North American industrial benchmarks.
Need Sample MTRs or Inspection Reports?
We provide complete EN 10204 3.1 Mill Test Certificates, PMI spectral logs, and optical aperture analysis sheets for any mesh specification.
Request Verified Stainless Steel Mesh Specifications
Submit target mesh counts, wire diameters, micron ratings, alloy requirements, or component drawings for review against international ASTM and ISO standards.